The resolution gap nobody mentions until it matters
FDM printing builds a part by melting filament through a nozzle and depositing it in lines, and the nozzle itself has a physical diameter, commonly around 0.4mm, that puts a hard floor on how fine a detail it can lay down. Resin printing works completely differently. A masked stereolithography printer cures liquid photopolymer using UV light projected through an LCD screen, and that screen is made up of thousands of tiny pixels, each one capable of curing resin independently. Consumer resin printers now commonly run 4K to 12K monochrome LCDs, which puts pixel size down in the range of 18 to 35 microns depending on the build volume of the machine.
That difference sounds abstract until you put an FDM print and a resin print of the same face next to each other. The FDM piece reads fine from a normal viewing distance, but lean in close and you'll see the layer lines, faint horizontal ridges running across the cheek or forehead. The resin piece doesn't have that problem at anywhere near the same scale. Eyelids, the philtrum above the lip, the subtle curve where a nostril meets the cheek, these are all features measured in fractions of a millimeter, and resin is the only additive process capable of holding that shape without it collapsing into a rounded approximation.
What actually happens after a resin print finishes
A resin print isn't done the moment the printer stops. It comes off the build plate soft, sticky, and still chemically uncured, sitting in a state that's neither liquid nor finished solid. It needs a wash, almost always in isopropyl alcohol, to strip away uncured resin still clinging to the surface, followed by a UV cure cycle that finishes hardening the material all the way through. Skip or shorten either step and the print stays tacky, doesn't hold color the same way once painted, and can warp slightly as it continues curing unevenly over time.
Support removal happens somewhere in that window too, usually after the wash but before the final cure, while the material still has a bit of give and is less likely to crack at the touchpoint. This is one of the reasons resin printing takes more total hands-on time than FDM even when the raw print itself finishes faster. FDM prints come off the plate essentially done. Resin prints come off the plate as the start of a second process.
Orientation decides more than people expect
How a model is angled on the build plate before slicing affects three things at once, and getting it wrong costs you on all three.
- Surface quality on the parts facing up versus down, since layer lines are least visible on surfaces angled away from the print direction
- Where supports are needed, and how many, since steeper overhangs need more support density
- Total print time, since taller orientations mean more layers even at the same layer height
We generally orient a face at an angle that keeps the front of it away from direct layer exposure, even when that means accepting a slightly longer print or a couple of extra support points somewhere less visible, like under the hairline or behind an ear.
Not all resin is the same resin
People sometimes assume resin printing means one material, the way filament printing gets shorthanded to "plastic." It doesn't. Standard resins are the most detail-capable but also the most brittle, fine for a static display piece that never gets handled roughly, less fine for anything with a thin protruding part likely to get bumped. Tough or ABS-like resins trade a small amount of surface detail for real impact resistance, which matters more on a piece with an outstretched arm or a weapon than people expect until one snaps. We pick the resin based on the geometry of the specific order, not a single default across every job.
Why we still use FDM for anything at all
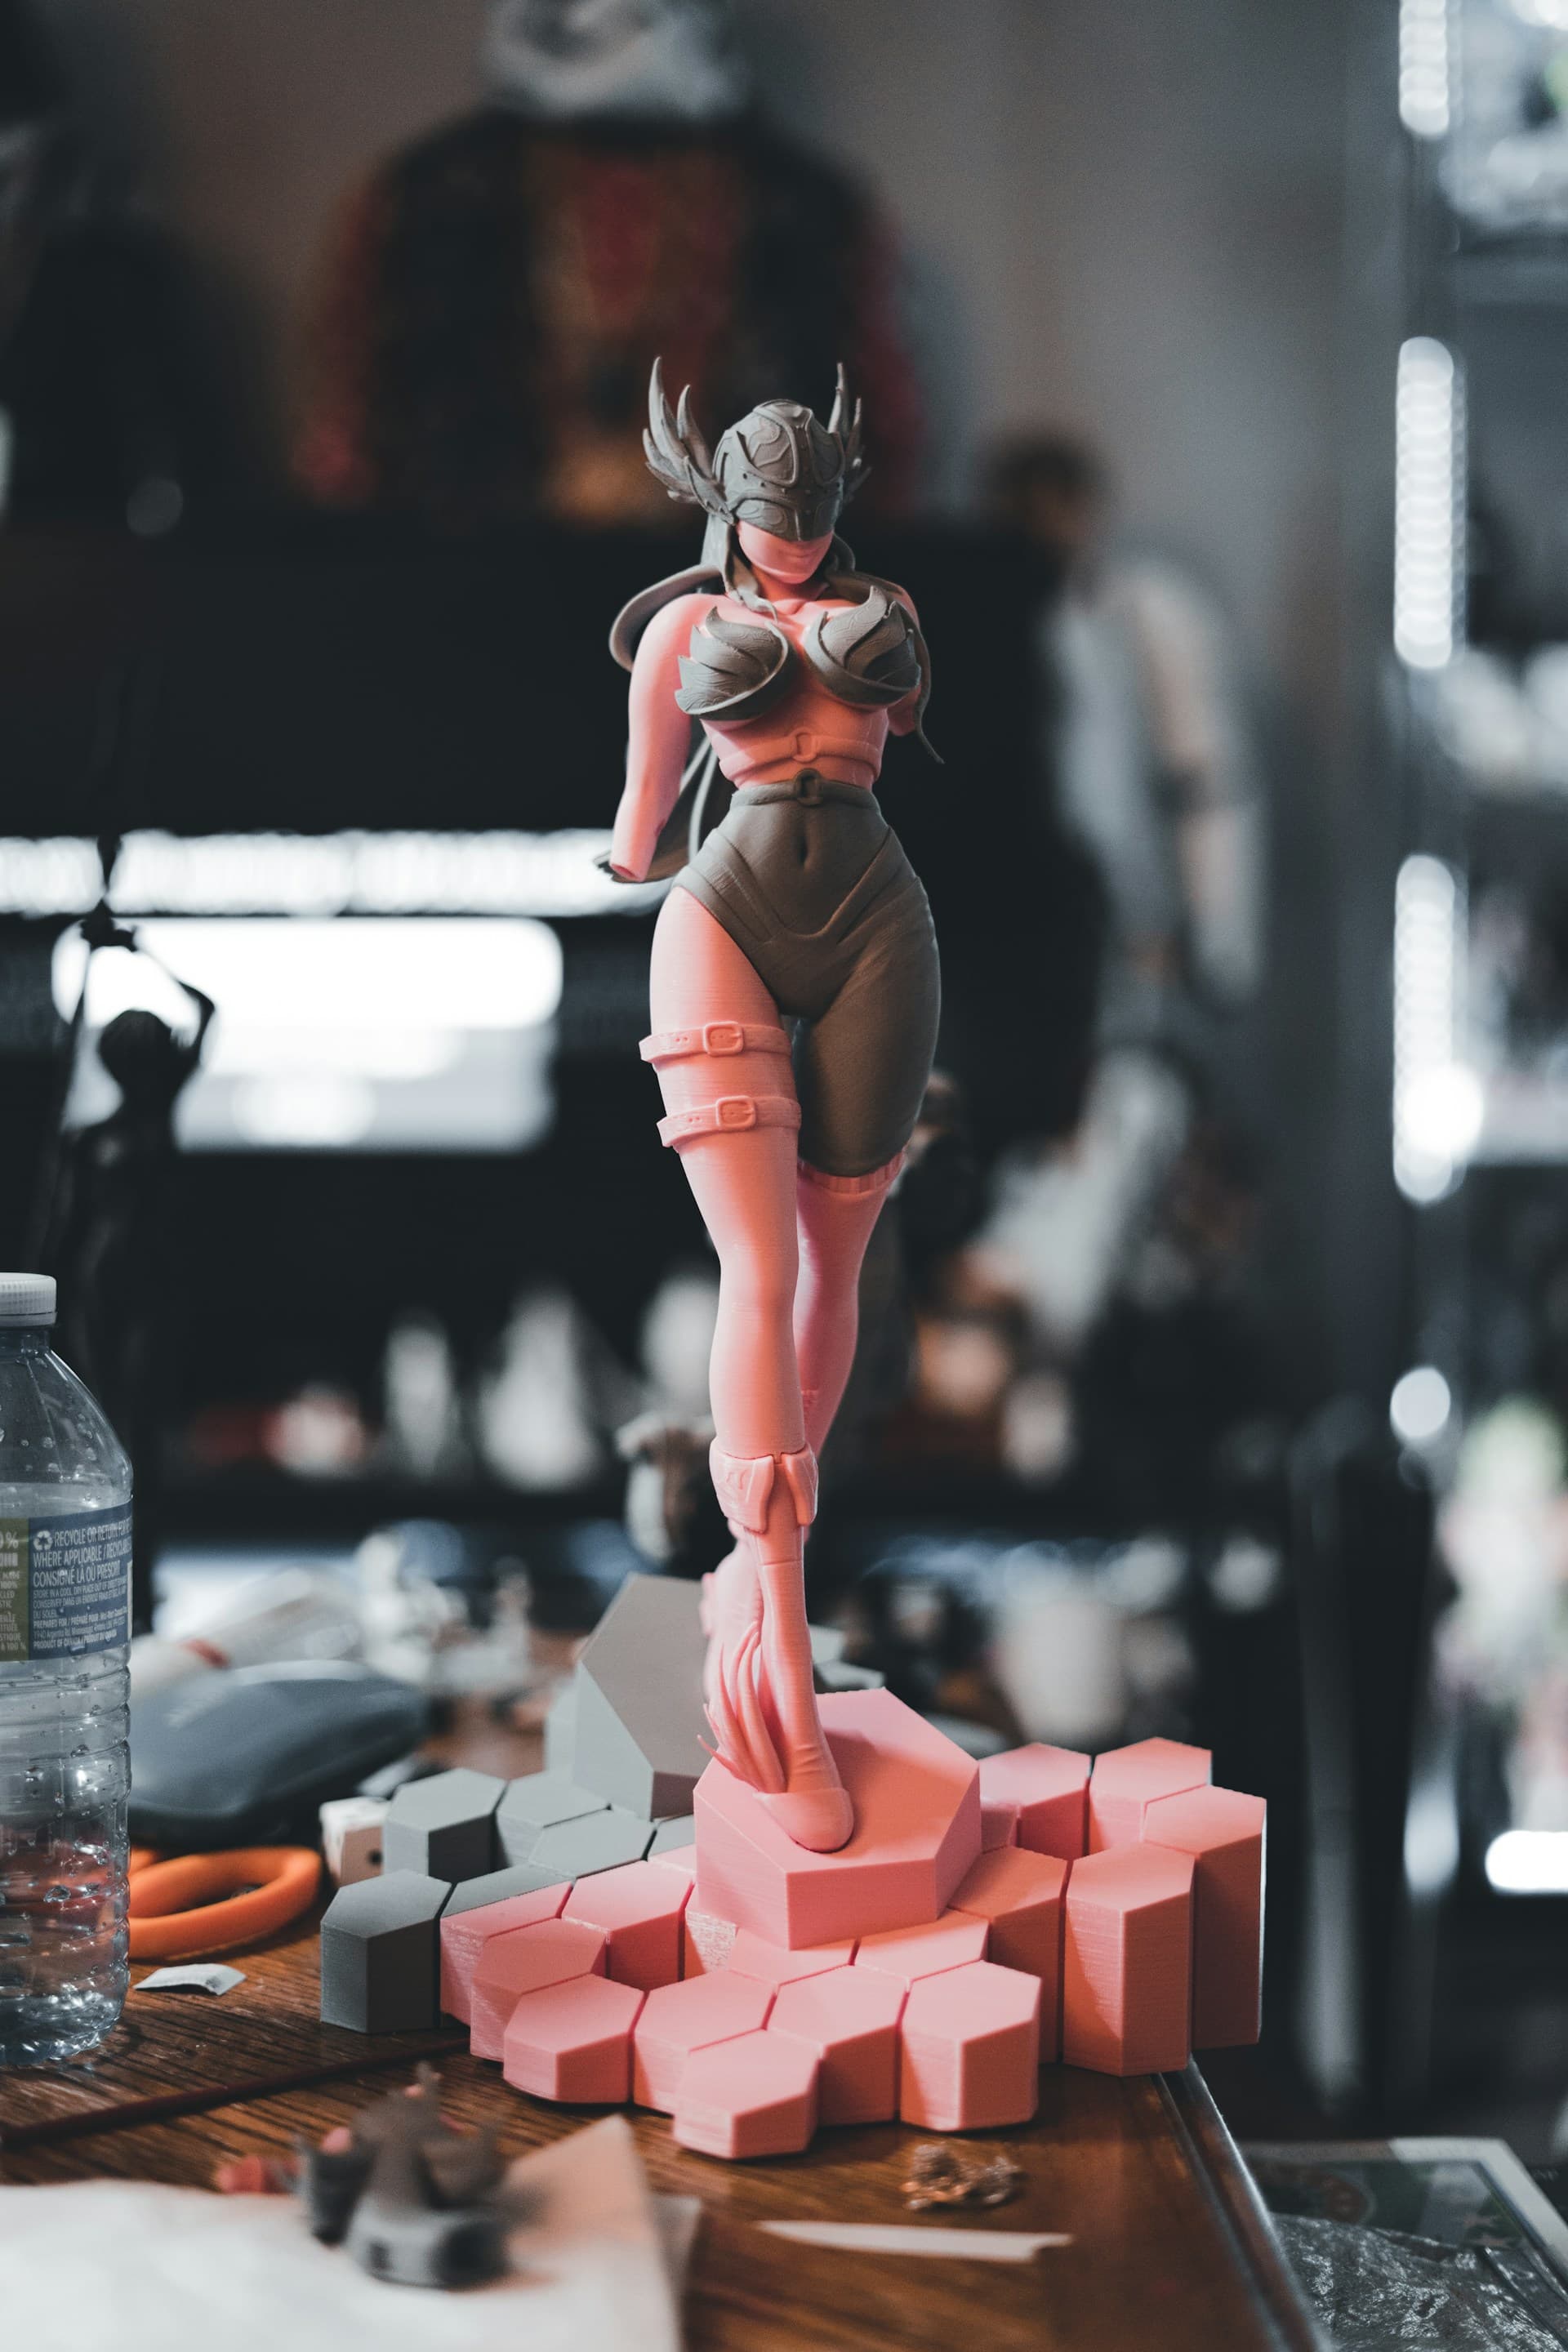
Given everything above, it's fair to ask why we don't just print everything in resin. Cost and scale are the honest answer. Resin is more expensive per milliliter than filament is per gram, build volumes on most resin printers are smaller, and larger pieces, especially our 6.8 and 8.4 inch sizes, would take significantly longer and cost more to produce entirely in resin without a proportional gain in visible quality on the larger surfaces that don't need micron-level precision. FDM handles bulk geometry efficiently. Resin earns its keep on the parts where a customer's eye actually goes first, which on almost every order is the face.
Using both isn't a compromise so much as matching the tool to what it's actually good at. A base or a large cloak doesn't benefit meaningfully from resin's resolution advantage. A face absolutely does, and that's where we spend the extra time and material cost every single order.
To see what this level of facial detail looks like once it's painted and finished, browse real customer orders on our reviews page, or start your own on the studio page.